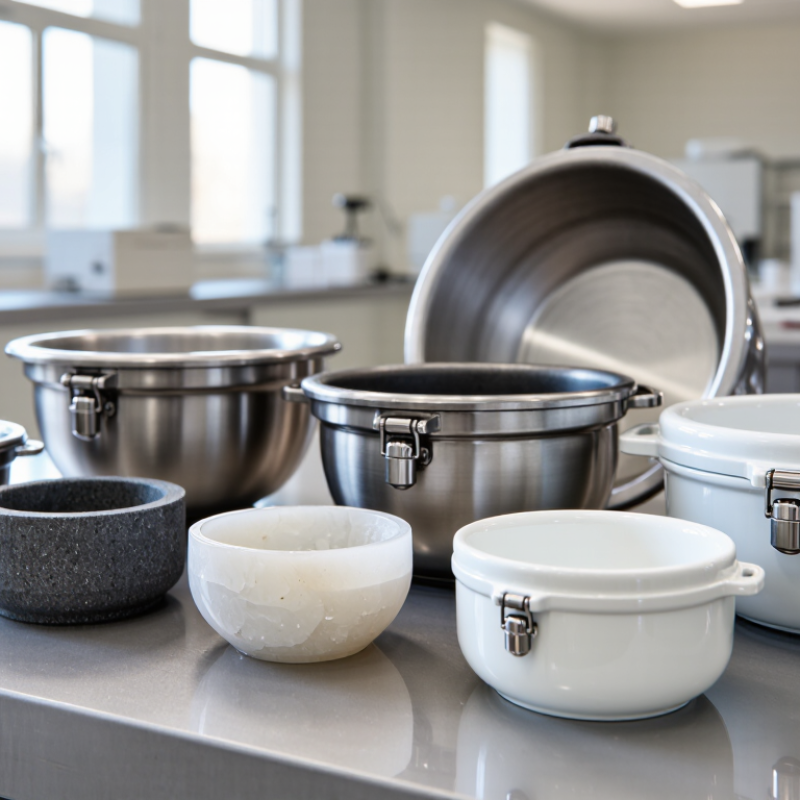
| Bowl body material | 304 stainless steel for general applications; 316 stainless steel for higher chloride or chemical exposure; alumina or zirconia for low-metal-contamination processing. | Material selection affects corrosion resistance, contamination risk, wear life, and cleaning performance. | Request the material grade, surface finish, chemical compatibility information, and material certificates where required. |
| Grinding or pulverizing medium | Use hardened steel for high-impact general work, ceramic for reduced metallic contamination, and tungsten-carbide components for very hard materials. | The medium determines achievable particle size, abrasion resistance, heat generation, and cross-contamination behavior. | Check hardness, density, replaceability, and compatibility with the sample chemistry. |
| Suitable sample type | Dry, brittle materials are generally easiest to pulverize; wet, fibrous, sticky, or elastic materials may require a specialized bowl and process. | Incorrect sample selection can cause clogging, poor size reduction, excessive heat, or rapid wear. | Conduct a representative sample test using the actual moisture content, hardness, and batch size. |
| Nominal and working capacity | Select a bowl whose working volume matches the application; laboratory bowls commonly range from tens to hundreds of millilitres, while process bowls may be measured in litres. | Overfilling reduces movement and pulverizing efficiency; underfilling can increase impact stress and uneven wear. | Confirm both nominal capacity and the manufacturer’s permitted working fill range. |
| Particle-size target | Choose the bowl and media according to the required final size; many laboratory pulverizing systems can produce fine powders, but actual results depend on feed size and material properties. | A stated target size is more useful than a generic “fine grinding” claim. | Require test data showing feed size, processing time, sample mass, and particle-size measurement method. |
| Heat management | Use intermittent operation, cooling intervals, or a temperature-controlled bowl when the sample is heat-sensitive or volatile. | Excessive temperature can alter moisture, damage organic materials, or create a safety hazard. | Ask for the allowable operating temperature, temperature-monitoring method, and duty-cycle limits. |
| Lid and containment | A secure, chemical-resistant lid with a reliable seal; use dust-tight containment for fine powders and hazardous samples. | Effective containment protects operators, reduces sample loss, and limits cross-contamination. | Check seal material, leak-test information, dust-control provisions, and compatibility with vacuum or inert-gas operation if needed. |
| Interlock and operator safety | The bowl should not operate unless correctly installed and securely closed; rotating or moving parts should remain inaccessible during operation. | Interlocks and guarding reduce the risk of contact, accidental opening, and sample ejection. | Verify documented risk assessment, emergency-stop function, guarding, and applicable local machinery requirements. |
| Dust and hazardous-material control | Use sealed transfer, local exhaust ventilation, suitable filtration, and a validated cleaning procedure for dusty, toxic, combustible, or allergenic powders. | Fine particles can present inhalation, contamination, and combustible-dust risks. | Obtain safety data, dust-emission information, grounding requirements, and any hazardous-area limitations before purchase. |
| Cleaning and sanitation | Prefer smooth, accessible surfaces, minimal crevices, removable contact parts, and validated cleaning instructions. | Good cleanability lowers carryover, microbial risk, downtime, and operator exposure. | Confirm whether parts tolerate water, detergents, solvents, ultrasonic cleaning, or autoclave cycles. |
| Wear inspection | Inspect the bowl, lining, lid, seals, and grinding media for cracks, deformation, pitting, thinning, or unusual surface loss. | Wear can change particle chemistry, introduce fragments, reduce capacity, and impair containment. | Set inspection intervals based on batch count, sample abrasiveness, and observed wear rather than calendar time alone. |
| Replacement parts | Seals, liners, lids, media, and fasteners should be individually replaceable and clearly identified. | Replaceable wear parts extend service life and reduce the cost of ownership. | Request part numbers, service life estimates, availability by region, and lead times. |
| Documentation and traceability | Technical drawings, operating instructions, material declarations, cleaning guidance, and inspection records should be available in English or the buyer’s required language. | Complete documentation supports safe commissioning, audits, training, and repeatable processing. | Confirm serial-number traceability, revision-controlled manuals, certificates, and export documentation. |
| Global logistics | Packaging should protect against impact, moisture, corrosion, and contamination during international transport. | Improper packaging can damage precision surfaces, seals, ceramic components, and calibration-critical parts. | Check shipping dimensions, customs classification, preservation method, inspection on arrival, and warranty coverage across borders. |
| Total cost of ownership | Evaluate purchase price together with media consumption, replacement parts, cleaning time, energy use, downtime, and disposal requirements. | The lowest initial price may not provide the lowest cost per processed batch. | Compare cost per kilogram or batch using a documented sample test and a defined maintenance schedule. |