| 1. Adhesive Selection | Two-component polyurethane adhesive | Usually supplied as Component A and Component B; 100% solids and no intentionally added organic solvent | Creates the bonding layer without a drying oven for solvent evaporation | Confirm compatibility with the film, foil, paper, ink, coating, and intended package contents |
| 2. Component A Preparation | Polyol or hydroxyl-functional resin component | Formulation-dependent; often the higher-volume component | Provides hydroxyl groups that react with the isocyanate component | Keep the material dry and maintain the specified temperature and viscosity |
| 3. Component B Preparation | Isocyanate-functional curing component | Formulation-dependent; commonly used at a lower proportion than Component A | Reacts with the polyol to form the polyurethane network | Protect from moisture because isocyanates react with water and can generate carbon dioxide |
| 4. Metering | Separate precision pumps | Mixing ratio is set by the adhesive formulation; common systems use a ratio near 100:50 to 100:100 by weight | Delivers the correct quantity of each component to the mixer | Verify ratio by weight, pump calibration, pressure, and flow stability |
| 5. Temperature Conditioning | Heated tanks, hoses, and application head | Often approximately 35–60 °C, depending on adhesive viscosity and equipment design | Reduces viscosity and supports uniform metering and coating | Use the adhesive supplier’s specified temperature limits; excessive heat can shorten usable life |
| 6. Mixing | Static mixer or dynamic mixing head | Continuous in-line mixing immediately before application | Combines the two reactive components into a homogeneous adhesive | Avoid unmixed streaks, air entrapment, dead zones, and excessive residence time |
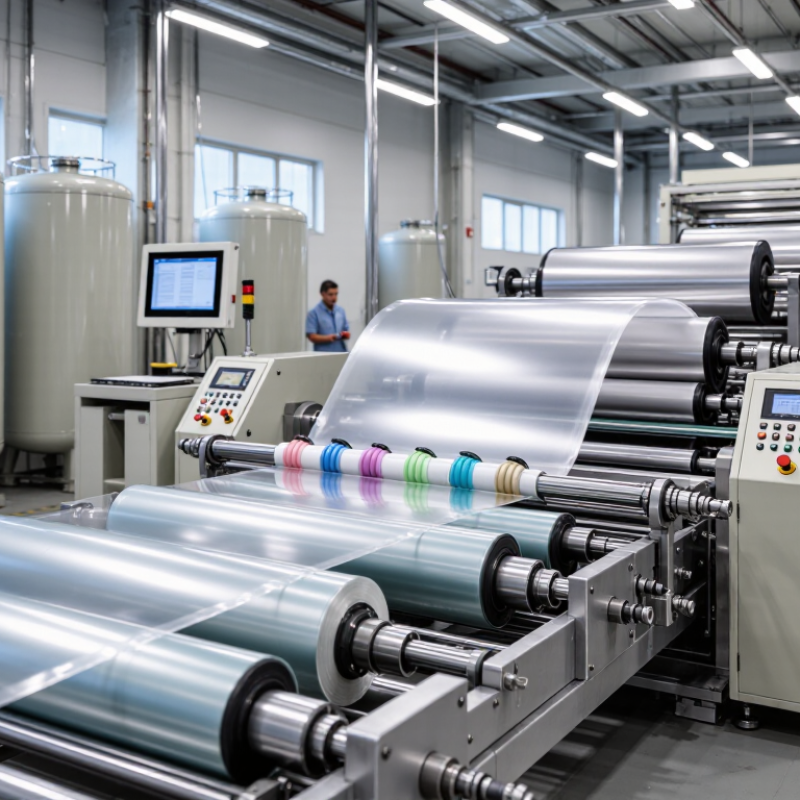
| 7. Adhesive Application | Gravure, smooth-roll, or other metering application system | Typical dry coating weight: about 0.8–2.5 g/m², depending on substrate and performance requirements | Deposits a thin, continuous adhesive layer on the web | Control coating weight, coverage, web tension, roll condition, and surface cleanliness |
| 8. Web Joining | Primary and secondary substrate | Examples include plastic film, metallized film, aluminum foil, paper, and coated structures | Brings the coated web into contact with the second substrate | Maintain nip pressure and alignment while avoiding wrinkles and trapped air |
| 9. Initial Bond Formation | Pressure-sensitive contact between layers | Immediate handling is possible in many systems, although final properties are not yet reached | Provides enough adhesion for winding, slitting, or further handling | Check for tunneling, bubbles, edge lift, blocking, and coating defects |
| 10. Curing | Polyurethane cross-linking reaction | Often requires several days for full cure; time depends on chemistry, temperature, humidity, and structure | Develops final bond strength, heat resistance, chemical resistance, and durability | Control storage temperature and avoid premature conversion before the specified cure time |
| 11. Quality Verification | Bond and appearance testing | Common checks include peel strength, visual inspection, coating weight, bond uniformity, and seal performance | Confirms that the laminate meets its intended functional requirements | Use test conditions appropriate for the substrate combination and end use |